
Ash Handling Systems for Biomass to Energy Boilers
Ash Handling Systems for Biomass-to-Energy Boilers
Biomass-to-energy boilers are used to convert organic materials like wood chips, agricultural waste, and other forms of biomass into heat and electricity. As a result of the combustion process, these boilers produce two primary types of ash: bottom ash and fly ash. Proper handling of these ashes is crucial to maintaining the efficiency of the boiler, ensuring compliance with environmental regulations, and minimizing maintenance costs.
In biomass power plants, ash handling systems must be designed to handle the specific characteristics of biomass ash, which can vary in terms of composition, temperature, and volume. These systems typically involve both wet and dry handling techniques, depending on the type of ash being processed and the specific needs of the plant.
Types of Ash in Biomass-to-Energy Boilers
- Bottom Ash
- Produced from the larger, heavier particles that fall to the bottom of the furnace.
- Typically, this ash is coarse and may contain inorganic materials that do not combust completely during the biomass burning process.
- Fly Ash
- Consists of finer particles that are carried away by the flue gases during combustion.
- This ash is often much lighter than bottom ash and can be more challenging to handle due to its fine nature and the potential for airborne emissions.
Ash Handling Technologies for Biomass Boilers
- Wet Ash Handling Systems
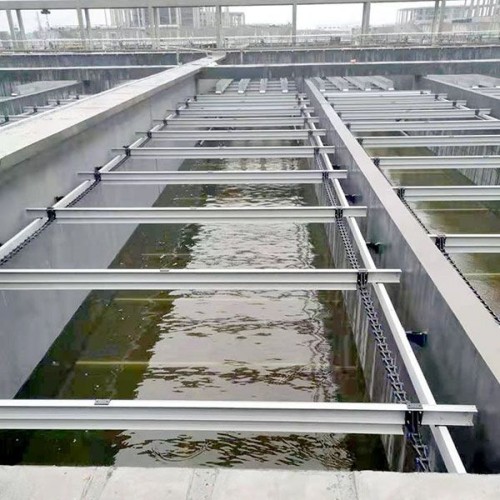
- Submerged Scraper Conveyors (SSC):
- Commonly used for bottom ash removal in biomass boilers.
- The ash is transported through a water-filled trough to cool it down and prevent dust formation. The submerged environment helps suppress ash particles and ensures safe transport.
- Advantages: Effective in cooling the ash, preventing dust emissions, and reducing wear on equipment due to the water lubrication.
- Disadvantages: Requires continuous water management and may not be suitable for all types of biomass ash due to moisture content.
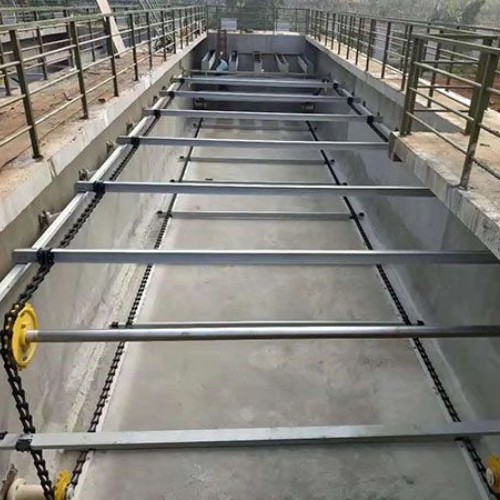
- Drag Chain Conveyors:
- Often used for conveying both bottom ash and fly ash in wet systems, especially for biomass boilers.
- Ash is transported through water or slurry to a collection area for further processing.
- Advantages: Low maintenance and can handle large quantities of ash. Suitable for handling large, coarse particles.
- Water Recirculation:
- Wet systems often use water recirculation to minimize fresh water usage while maintaining ash cooling and dust suppression.
- Benefits: Reduced operational costs by reusing water; ensures continuous operation.
- Submerged Scraper Conveyors (SSC):
- Dry Ash Handling Systems
- Pneumatic Conveying Systems:
- Fly ash is typically conveyed using pneumatic conveying systems, where air or vacuum is used to transport fine ash particles.
- These systems are ideal for biomass boilers producing fine fly ash due to the lightweight, fine particulate nature of biomass ash.
- Advantages: Dust suppression, ability to handle long-distance ash transport, and flexible system design.
- Disadvantages: Can require additional energy for pneumatic transport and maintenance of air filtration systems.
- Mechanical Chain or En-Masse Conveyors:
- Chain conveyors or en-masse conveyors can be used in dry systems for biomass bottom ash removal. These conveyors are designed to handle both coarse and fine materials, depending on the configuration.
- Advantages: High capacity, robust design, and efficient for handling large volumes of ash.
- Disadvantages: Requires more maintenance than wet systems, especially when handling fine fly ash.
- Vacuum Conveyors:
- Vacuum systems are another option for conveying fly ash in a dry format. They are particularly effective at capturing airborne ash and minimizing dust emissions during transport.
- Advantages: Excellent dust control and efficient ash collection.
- Disadvantages: Can be more complex and require higher initial investment.
- Pneumatic Conveying Systems:
Key Features of Ash Handling Systems for Biomass Boilers
- Dust Control and Emission Management
- Biomass-to-energy plants often burn materials that generate fine ash, which can become airborne during transport. A well-designed ash handling system incorporates dust suppression measures such as water sprays, vacuum collection, and air filtration.
- Regulations: Biomass plants are subject to strict environmental regulations, making effective dust control a priority to ensure compliance with emission standards.
- Temperature Control
- Bottom ash from biomass boilers can be very hot. Cooling systems like wet conveyors or air-cooling techniques help prevent damage to conveyor components and reduce fire risks.
- Thermal shock resistance in the system design is important to handle the high temperatures of biomass combustion byproducts.
- Handling Mixed Ash Streams
- Biomass ash can vary in composition depending on the feedstock (e.g., wood, agricultural waste). A good ash handling system can handle mixed ash streams effectively, with capabilities to separate bottom ash from fly ash and transport them to their respective processing or disposal areas.
- Efficiency and Automation
- Automated controls and sensors ensure efficient operation by monitoring ash levels, water quality (in wet systems), and conveyor speeds. This improves system performance and reduces the risk of human error.
- Energy efficiency is a key consideration, particularly in dry systems where energy is used for pneumatic transport and filtration.
Advantages of Ash Handling Systems for Biomass-to-Energy Boilers
- Environmental Compliance
- Effective dust control and emission management ensure that the plant adheres to environmental standards, preventing pollutants like particulate matter from being released into the atmosphere.
- Reduced Maintenance Costs
- Wet systems, especially submerged scraper conveyors, experience less wear and tear compared to dry systems, reducing the frequency of repairs and associated costs.
- Improved Operational Efficiency
- Well-designed ash handling systems increase the overall efficiency of biomass boilers by keeping ash from accumulating in the combustion chamber and ensuring continuous removal and disposal of waste byproducts.
- Energy and Water Conservation
- Water recirculation systems in wet systems reduce water consumption, and automated control systems optimize energy use in pneumatic or mechanical systems, leading to more cost-effective operations.
- Safety
- Systems that handle hot ash and fine fly ash with dust suppression features reduce the risk of fire hazards, explosions, and health risks to plant workers due to inhalation of fine particles.
Challenges of Ash Handling Systems in Biomass-to-Energy Boilers
- Variability in Ash Composition
- The composition of biomass ash can vary significantly depending on the biomass feedstock, which can affect the design of the handling system. For example, ash from wood chips may have different properties than ash from agricultural residues.
- Solution: Ash handling systems need to be adaptable, often incorporating multiple technologies (wet and dry) to handle different types of ash.
- Water and Energy Management
- Wet systems require careful management of water to avoid excessive consumption and ensure the proper cooling of bottom ash. Similarly, pneumatic systems may require additional energy for air compression and filtration.
- Solution: Implement efficient water recirculation and energy recovery practices to minimize resource consumption.
- Space Constraints
- The installation of wet ash handling systems often requires more space due to the need for water troughs, tanks, and filtration systems, while dry systems can also take up considerable space with pneumatic equipment.
- Solution: Optimize the layout of ash handling systems and consider modular, space-efficient designs.
Conclusion
Effective ash handling systems are essential for maintaining the performance, safety, and environmental compliance of biomass-to-energy boilers. Whether through wet systems (such as submerged scraper conveyors) or dry systems (such as pneumatic conveyors or mechanical conveyors), the system must be designed to handle both bottom ash and fly ash efficiently, safely, and with minimal environmental impact.
Key considerations include managing dust emissions, cooling hot ash, ensuring efficient water and energy use, and accommodating the varying ash compositions produced by different biomass feedstocks.
A well-designed ash handling system improves operational efficiency, lowers maintenance costs, and supports the long-term success of biomass-to-energy plants. If you’re looking to integrate or optimize an ash handling solution, ensure that the system is flexible, energy-efficient, and environmentally friendly to meet the unique needs of your biomass boiler.
Mechanical Ash Handling System | Ash Handling System | Types of Ash Handling System |
Bottom and fly ash handling systems
“REDLER” CHAIN CONVEYORS
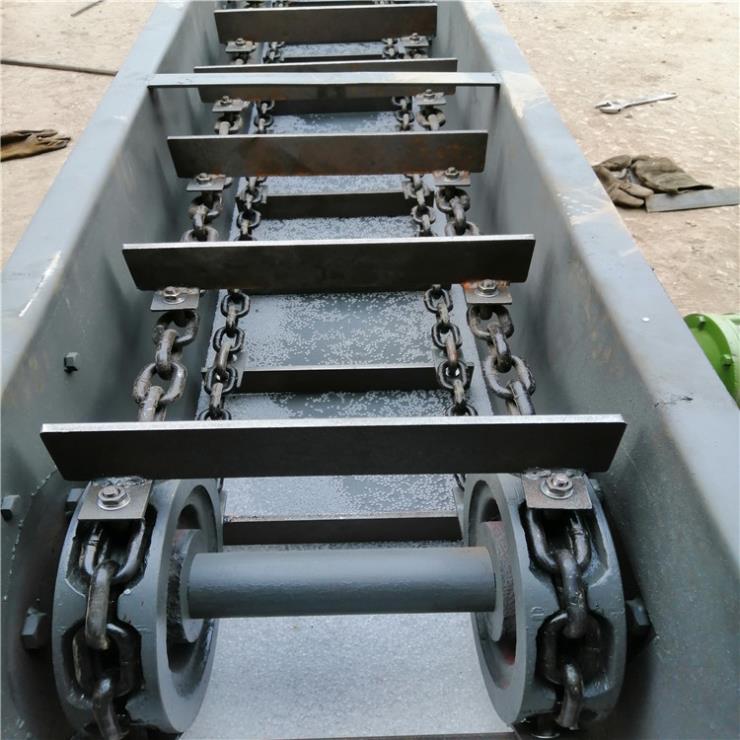
The “REDLER” chain conveyor is ideal for transporting all sorts of granulated products (cereals, seeds, wood chips, pomace extracts, etc.) efficiently and over long distances, either horizontally or at an incline. They are manufactured in a modular form, are easy to assemble and have low maintenance requirements. Its drive system can be driven directly or by chain, according to the required technical characteristics.
Its watertight design means that it never produces spills and at the same time prevents rain and external weather effects from coming into contact with the product. The product is conveyed by single or double drag chains, depending on the application.
The chain conveyor (redler) is used to transport different types of powder and granular materials, most commonly used when we have long distances or high loads for transport in hoppers (in this case, working drowned) and in combined horizontal and inclined transport.
The Redler conveyor or drag chain, is mainly characterized for its great capacity for, preferably, horizontal transport over long distances of a high percentage of bulk materials, that could be: cereals, seeds, flours and definitively any grain product, allowing unloading throughout its length, adapting to different processes.
Description
They have a robust chassis, low internal friction, the sprocket is split and manufactured in a special alloy, which allows maintenance without removing the shaft, guides and drag plates made in uhmw, ensuring hygiene and high durability, with the possibility of being hermetically sealed for processes that are even more demanding.
Due to our expertise, we are able to manufacture chain conveyors in horizontal and inclined positions for various types of products, also adding coverage and adaptations for the suction of the entire process when necessary, the filtered product can be directed to any location desired by the customer, thus providing a lossless and very efficient transport process.
Application
It is widely used in products such as: grains, flour, feed, chips, ash, cement, other more viscous and aggressive products such as sugar and urea the stainless steel design can be used.
A water-sealed scraper conveyor is a specialized type of conveyor system used in waste incineration and other industrial processes where managing dust, fumes, and residue is crucial. Here’s a detailed look at how it works and its applications:
### **Components and Function**
1. **Conveyor Belt**: This is the main component of the conveyor system. It’s typically made of durable materials like steel or reinforced rubber to handle the harsh conditions in an incineration plant.
2. **Scraper Mechanism**: Scrapers are attached to the conveyor belt to remove residual materials such as ash or waste products that accumulate on the belt. This helps maintain the efficiency of the conveyor and prevents clogging.
3. **Water Seal**: The water seal is a key feature of this conveyor system. It involves a trough or chamber where water is used to create a seal that prevents gases, dust, and particulate matter from escaping into the atmosphere. The water also helps cool the conveyor components and manage temperature fluctuations.
### **How It Works**
- **Waste Handling**: Waste material is fed onto the conveyor belt. As the belt moves, the scraper mechanism ensures that any residues are continuously removed and managed.
- **Dust and Emissions Control**: The water seal helps to control dust and emissions by creating a barrier that captures and contains airborne particles and gases. The water in the seal can also trap and cool any hot gases that might otherwise escape.
- **Ash Removal**: In incineration plants, ash is a byproduct of the burning process. The scraper conveyor system moves the ash to designated collection areas, ensuring that it’s efficiently removed from the furnace area.
- **Maintenance**: The water seal system also helps reduce the wear and tear on the conveyor belt and associated machinery by preventing the buildup of hot or corrosive residues.
### **Applications**
- **Waste Incineration Plants**: In these facilities, a water-sealed scraper conveyor is used to handle and transport waste, manage byproducts, and control emissions.
- **Power Plants**: Beyond waste incineration, similar systems are used in power plants to handle ash and other residues from combustion processes.
- **Industrial Processes**: Any industrial process that involves the handling of particulate materials or requires emission control may use a water-sealed scraper conveyor.
### **Benefits**
- **Enhanced Safety**: By controlling dust and fumes, the system helps maintain a safer working environment.
- **Improved Efficiency**: Continuous removal of residues and effective emission control contribute to the overall efficiency of the incineration process.
- **Reduced Maintenance**: The water seal helps prevent excessive wear on the conveyor system, leading to lower maintenance costs and longer equipment life.
- **Environmental Compliance**: Helps meet environmental regulations by controlling emissions and reducing the release of harmful substances into the atmosphere.
### **Considerations**
- **Water Management**: Proper management of the water seal system is essential to ensure its effectiveness and prevent issues like clogging or overflow.
- **Maintenance Requirements**: Regular maintenance is needed to ensure the scraper mechanism and water seal are functioning correctly and to address any wear or damage.
Overall, a water-sealed scraper conveyor is a crucial component in managing the complex needs of waste incineration and similar processes, combining material handling with emissions control.
SELECTION & TECHNICAL QUESTIONS
Q1: How do I select the right conveyor model? What information should I provide?
> To recommend the most suitable solution, please provide the following details:
> 1. Material type: What material are you conveying? (e.g., fly ash, wood chips, biomass pellets, bottom ash, etc.)
> 2. Material properties: Particle size, temperature, moisture content, abrasiveness
> 3. Capacity requirement: How many tons per hour (t/h) do you need?
> 4. Installation conditions: Conveying distance, incline angle, space limitations
> 5. Application industry: Which industry is this for? (e.g., waste-to-energy plant, biomass power plant, cement plant)
> You can also email us or contact us via WhatsApp. Our engineers will get back to you within 24 hours.
Q2: What is the difference between screw conveyors and chain conveyors? Which one should I choose?
> Both types have different applications:
> – Screw Conveyors: Best for powdery and small-grain materials (e.g., fly ash, cement powder). Good sealing performance, simple structure, low maintenance cost.
> – Chain Scraper Conveyors: Best for bulky, highly abrasive materials (e.g., bottom ash, municipal solid waste, biomass fragments). Supports multiple inlet and outlet points.
> – Bucket Elevators: Ideal for vertical or steep-incline material lifting.
> If you are not sure, tell us your material and working conditions, and our engineers will help you choose.
Q3: Can your equipment handle high-temperature materials? What is the maximum temperature?
> We can customize equipment according to material temperature:
> – Standard type: 0~80°C, carbon steel
> – Medium temperature type: 80~200°C, thickened wear-resistant liner
> – High temperature type: 200~400°C, special heat-resistant steel, optional cooling jacket
> Please tell us your material temperature, and we will recommend the most suitable material solution.
Q4: Are there any limits on conveying distance and lifting height?
> Standard design range:
> – Screw conveyor: Single section up to 70 meters; multiple sections can be connected for longer distances
> – Chain conveyor: Single machine up to 60 meters
> – Bucket elevator: Lifting height up to 50 meters
> We can also customize for extra-long distances or special angles. Contact us for detailed solutions.
Q5: Do you provide explosion-proof design?
> Yes. For explosive and flammable conditions such as pulverized coal and biomass dust, we offer:
> – Explosion-proof motors (Ex d IIB T4 standard)
> – Reserved openings for explosion vents / rupture discs
> – Fully sealed structure to prevent dust leakage
> Please specify your explosion-proof rating requirements.
CUSTOMIZATION & MANUFACTURING
Q6: Do you support customization? What is the lead time?
> Over 90% of our equipment is customized according to customer working conditions. Standard models take about 90–120days. Special customizations take 120–180 days, depending on configuration complexity.
Q7: What material options do you offer?
> Common materials include:
> – Carbon steel (Q235B): Standard working conditions
> – Wear-resistant steel (NM400/NM500): Highly abrasive materials
> – Stainless steel 304/316L: Food, chemical, corrosion-resistant requirements
> – Bi-metal wear-resistant composite plate: Extreme abrasion conditions
> We will recommend the most cost-effective material solution based on your material properties.
Q8: What certifications do you have?
> We hold the following certifications:
> – ISO 9001:2015 Quality Management System
> – ISO 14001 Environmental Management System
> – ISO 45001 Occupational Health & Safety Management
> – CE Certification (EN 1090 Steel Structure)
> If you need scanned copies of specific certificates, please contact us.
DELIVERY & LOGISTICS
Q9: Which countries do you export to? Do you have export experience?
> Our equipment has been exported to more than 20 countries worldwide, including:
> – Europe: Germany, France, Poland, Turkey, etc.
> – Southeast Asia: Singapore, Thailand, Indonesia, Vietnam, etc.
> – Middle East: Saudi Arabia, UAE, etc.
> – South America**: Brazil, Chile, etc.
> We are familiar with the full export process: packaging, customs declaration, and ocean freight. We can provide FOB, CIF, and other trade terms.
Q10: What is your packaging method? Is it suitable for long-distance ocean shipping?
> Export-standard packaging:
> – Large items / complete machines**: Rust prevention + waterproof film + fumigated solid wood pallet
> – Precision components: Wooden case with shock-absorbing filling
> – Random accessories: Categorized packing with detailed packing list
> All wooden packaging meets IPPC fumigation standards for direct customs clearance.
Q11: What is your minimum order quantity?
> We do not have a strict minimum order quantity. Single-unit orders are welcome. Bulk orders can enjoy more favorable pricing.
INSTALLATION & AFTER-SALES
Q12: Do you provide installation guidance? Do engineers need to come to site?
> We offer two service options:
> 1. Remote guidance: Detailed installation drawings and operation manuals, video guidance for installation (free of charge)
> 2. On-site service: Dispatch engineers to site for installation and commissioning (travel costs are additional)
> Most customers choose remote guidance. Our equipment is designed as a modular structure for easy installation.
Q13: What is the warranty period? What are the wearing parts?
> Standard warranty period is 12 months (from the date of arrival at port).
> Wearing parts list:
> – Chain / screw flights: Approximately 1–3 years, depending on material abrasiveness
> – Liners: Approximately 2–4 years
> – Bearings: Approximately 2–3 years
> We recommend ordering a wearing-parts spare kit together with your first order.
Q14: How do you solve problems during operation?
> We provide 7×24 technical support:>
> – Response within 24 hours for technical issues
> – Remote video troubleshooting guidance
> – Engineer on-site service when necessary
> – Common spare parts in stock for fast delivery
QUOTATION & COOPERATION
**Q15: How can I get a quote? How long does it take?
> Quotation process:
> 1. You provide material parameters, capacity, installation conditions, and other requirements
> 2. Our engineers evaluate and select the appropriate model
> 3. Formal quotation and technical proposal provided within 7 working days
> You can contact us via email, or the online inquiry form.
Q16: What are your payment terms?
> Standard payment terms:
> – 30% advance payment: After contract signing, to start production
> – 70% balance: Before shipment, or against copy of Bill of Lading
For long-term cooperative customers, more flexible payment terms can be negotiated.
Follow these 3 steps to find your ideal conveyor solution
Step 1: Identify Your Material Type
Different materials require different conveyor designs. Tell us what you are conveying:
| Material Category | Examples | Recommended Conveyor Type |
| Powder / Fine Granules | Fly ash, cement powder, lime powder | Screw Conveyor |
| Small Granules / Pellets | Biomass pellets, plastic granules, grain | Screw Conveyor / Belt Conveyor |
| Fragments / Chips | Wood chips, bark, agricultural residues | Chain Scraper Conveyor |
| Bulky / Abrasive | Bottom ash, slag, MSW, clinker | Chain En-Masse Conveyor |
| Vertical Lift | Any bulk material needs vertical transport | Bucket Elevator |
Step 2: Define Your Working Conditions
Please prepare the following parameters before contacting us:
| Parameter | Why It Matters | Example |
| Capacity (t/h) | Determines conveyor size and power | 10 t/h, 50 t/h, 100 t/h |
| Conveying Distance (m) | Determines machine length | 15m horizontal, 30m incline |
| Incline Angle (°) | Affects capacity and design | 0° horizontal, 30° incline |
| Material Temperature (°C) | Determines material grade | Ambient, 150°C, 300°C |
| Moisture Content (%) | Affects discharge design | Dry, damp, wet (needs dewatering) |
| Abrasiveness | Determines liner thickness | Low, medium, high |
| Application Industry | Determines certification needs | Power plant, cement, mining, recycling |
Step 3: Choose Configuration Options
Based on your answers above, our engineers will recommend:
Material grade — carbon steel / wear-resistant steel / stainless steel
Sealing type — open trough / fully enclosed / gas-tight
Drive system — motor power, gearbox brand, speed range
Auxiliary options — explosion-proof motor, cooling jacket, cleaning device, level sensors
Not Sure Where to Start?
Send us your basic requirements, and our engineers will design a customized solution for you — completely free.
Email: bootec@bootecgroup.com Response time: Within 24 hours
[REQUEST A FREE QUOTATION →]