
Submerged Scraper Conveyors For bottom ash handling
Submerged Scraper Conveyors for Bottom Ash Handling
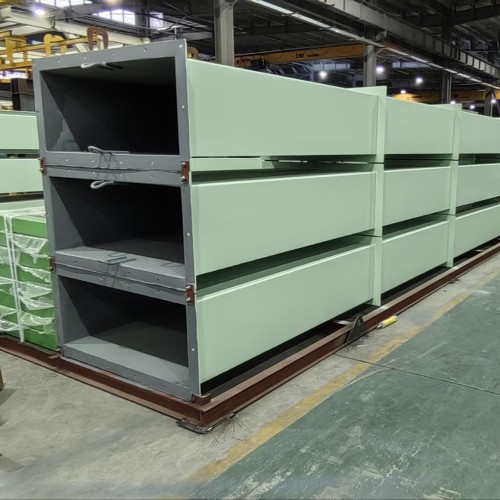
Submerged Scraper Conveyors (SSCs) are widely used in coal-fired power plants and waste-to-energy facilities for the efficient and safe handling of bottom ash produced during combustion processes. These systems combine the advantages of a submerged conveyor design with a scraper mechanism to transport bottom ash through water-filled channels. The scraper system, in particular, ensures effective removal of ash from the boiler and reduces the potential for clogging, wear, and dust emissions.
Key Features of Submerged Scraper Conveyors (SSCs)
- Water-Cooled Design:
- The conveyor operates submerged in water, which helps cool the hot bottom ash immediately after it is removed from the boiler. This cooling reduces the risk of fires and dust emissions, while also protecting conveyor components from heat damage.
- Scraper Mechanism:
- The scraper system consists of a series of scraper blades attached to a chain that moves along the trough. The scrapers scrape the ash off the bottom of the trough and move it toward the discharge area, ensuring that even dense, sticky ash is effectively transported.
- Heavy Duty Construction:
- SSCs are built with robust materials that can withstand the abrasive nature of bottom ash and the high temperatures associated with its handling. Common materials include stainless steel or high-strength alloys, which offer durability and corrosion resistance.
- Dust Suppression:
- The submerged design prevents ash dust from becoming airborne, offering significant benefits in terms of environmental and workplace safety.
- Efficient Ash Transport:
- SSCs can handle large quantities of bottom ash quickly and efficiently. The continuous operation of the conveyor ensures that ash is removed from the combustion area without causing delays in the plant’s operations.
- Corrosion and Abrasion Resistance:
- Given the harsh conditions in which SSCs operate (high temperatures, water, and abrasive ash), the conveyor’s materials are selected to minimize wear and corrosion.
Working Principle of Submerged Scraper Conveyors
- Ash Collection from the Boiler:
- Bottom ash is collected as it is ejected from the boiler or combustion chamber. The ash is typically removed via discharge hoppers or slag taps and directed into the submerged scraper conveyor system.
- Transport Through the Submerged Trough:
- The bottom ash flows into a water-filled trough, where the scraper conveyor system is located. The scrapers (attached to a moving chain) scrape the ash from the bottom of the trough and move it along the length of the system.
- Scraping and Moving Ash:
- The scrapers work in conjunction with the chain, which drives them forward. As the ash is moved along the trough, it is kept submerged in water, cooling it down and suppressing any potential dust generation.
- Discharge of Ash:
- At the end of the submerged conveyor system, the bottom ash is discharged either into a cooling pit, storage hopper, or other designated disposal area. The discharge point may be equipped with a sluicing system to further cool and manage the ash.
- Water Circulation and Maintenance:
- The water used to submerge the conveyor is continuously circulated, ensuring that the ash remains cool and that the system functions effectively. The water system should be regularly maintained to prevent clogging and maintain proper flow.
Advantages of Submerged Scraper Conveyors for Bottom Ash Handling
- Dust-Free Operation:
- The submerged system significantly reduces the likelihood of dust generation, making it a cleaner and safer solution for bottom ash handling compared to dry systems.
- Efficient Cooling of Ash:
- The water in the submerged trough cools the hot bottom ash, preventing excessive heat build-up and protecting both the ash and the conveyor system from heat-related damage.
- Handling of Dense Ash:
- The scraper mechanism is particularly effective at handling dense, sticky, or clumped bottom ash, ensuring that the material is moved efficiently without the risk of clogging or blockages.
- Reduced Wear and Tear on Conveyor Components:
- By keeping the ash submerged in water, the abrasive effects on the conveyor components (such as chains and flights) are reduced, leading to lower maintenance costs and extended equipment lifespan.
- Enhanced Safety and Reliability:
- The system is designed to handle high temperatures, abrasive materials, and heavy ash loads. This makes it suitable for continuous operation, ensuring a reliable and safe ash handling process.
- Environmental and Regulatory Compliance:
- The submerged design helps comply with environmental regulations by reducing the release of ash dust and particulate matter into the air, minimizing the plant’s environmental footprint.
- Low Maintenance Requirements:
- The submerged environment helps protect the system from external damage, reducing the frequency of repairs and extending the overall life of the equipment.
Components of a Submerged Scraper Conveyor System
- Submerged Trough:
- A water-filled channel where the bottom ash is transported. The trough helps cool the ash and suppresses dust emissions while preventing it from becoming airborne.
- Scraper Mechanism (Scraper Blades):
- The scrapers are attached to a chain that moves along the trough. The scrapers are responsible for lifting and transporting the ash as it moves along the conveyor. They are designed to effectively handle the dense, sticky nature of bottom ash.
- Chain and Drive Mechanism:
- The scraper blades are connected to a chain that is driven by a motorized drive system. The drive unit ensures continuous motion of the conveyor and the scrapers.
- Water Circulation System:
- The water in the trough is constantly circulated to maintain the cooling effect and prevent the build-up of contaminants. A proper circulation system is essential to ensure the efficiency of the submerged conveyor.
- Ash Discharge System:
- At the end of the conveyor, the ash is discharged. The discharge system can include a sluicing mechanism to direct the cooled ash into storage or disposal containers.
- Inspection and Maintenance Ports:
- Ports are provided to allow for periodic inspection and maintenance of the system. This ensures the scrapers, chain, and water circulation system continue to function optimally.
Applications of Submerged Scraper Conveyors
- Coal-Fired Power Plants:
- In these plants, submerged scraper conveyors handle the bottom ash produced from burning coal. The system efficiently moves large volumes of ash from the boiler to the storage or disposal area.
- Waste-to-Energy Plants:
- Waste-to-energy plants use submerged scraper conveyors to process and transport the bottom ash produced during the incineration of municipal solid waste.
- Cement Production:
- Submerged scraper conveyors can be used in cement plants to handle bottom ash produced from the combustion of waste materials in rotary kilns.
- Metallurgical Plants:
- Steel mills and other metallurgical facilities use these conveyors to handle slag and other byproducts generated during the melting or refining of metals.
- Incineration Facilities:
- In waste incineration facilities, submerged scraper conveyors are employed to handle and transport the ash left behind after combustion.
Maintenance Considerations for Submerged Scraper Conveyors
- Water Quality Monitoring:
- The water used in the submerged system should be regularly checked to ensure that it remains free of contaminants, which could impede the cooling and ash transport processes.
- Wear and Tear on Scrapers and Chain:
- The scraper blades and conveyor chain should be inspected for wear and damage, as the abrasive nature of bottom ash can lead to component degradation over time.
- Regular Inspection of the Drive Mechanism:
- The drive system, which powers the conveyor chain and scrapers, should be checked periodically for efficiency, ensuring that there are no signs of excessive wear or malfunction.
- Cleaning and Lubrication of the Conveyor Components:
- Regular cleaning of the submerged conveyor system and lubrication of moving parts are essential to ensure smooth operation and extend the lifespan of the equipment.
- Inspecting the Water Circulation System:
- The water circulation system should be regularly inspected and cleaned to ensure that water flow is maintained, preventing blockages and maintaining the cooling effect.
Why Choose Submerged Scraper Conveyors for Bottom Ash Handling?
- Effective Dust Control:
- The submerged system eliminates airborne dust, reducing health risks and maintaining a cleaner environment around the plant.
- Efficient Ash Cooling and Transport:
- The water-filled trough ensures that bottom ash remains cool during transport, while the scraper mechanism efficiently moves even dense ash.
- Durability and Reliability:
- Submerged scraper conveyors are designed to handle the abrasive and high-temperature conditions of bottom ash handling, ensuring a long lifespan with minimal maintenance.
- Environmental Compliance:
- By controlling dust emissions and reducing the environmental impact, submerged scraper conveyors help meet regulatory requirements for air quality.
- Cost-Effective Solution:
- The reduced need for maintenance and the system’s longevity make submerged scraper conveyors a cost-effective solution for power plants and waste-to-energy facilities.
If you need more details on how to implement or design a Submerged Scraper Conveyor for your bottom ash handling needs, feel free to reach out!
Submerged Chain Conveyor System For bottom ash handling

SELECTION & TECHNICAL QUESTIONS
Q1: How do I select the right conveyor model? What information should I provide?
> To recommend the most suitable solution, please provide the following details:
> 1. Material type: What material are you conveying? (e.g., fly ash, wood chips, biomass pellets, bottom ash, etc.)
> 2. Material properties: Particle size, temperature, moisture content, abrasiveness
> 3. Capacity requirement: How many tons per hour (t/h) do you need?
> 4. Installation conditions: Conveying distance, incline angle, space limitations
> 5. Application industry: Which industry is this for? (e.g., waste-to-energy plant, biomass power plant, cement plant)
> You can also email us or contact us via WhatsApp. Our engineers will get back to you within 24 hours.
Q2: What is the difference between screw conveyors and chain conveyors? Which one should I choose?
> Both types have different applications:
> – Screw Conveyors: Best for powdery and small-grain materials (e.g., fly ash, cement powder). Good sealing performance, simple structure, low maintenance cost.
> – Chain Scraper Conveyors: Best for bulky, highly abrasive materials (e.g., bottom ash, municipal solid waste, biomass fragments). Supports multiple inlet and outlet points.
> – Bucket Elevators: Ideal for vertical or steep-incline material lifting.
> If you are not sure, tell us your material and working conditions, and our engineers will help you choose.
Q3: Can your equipment handle high-temperature materials? What is the maximum temperature?
> We can customize equipment according to material temperature:
> – Standard type: 0~80°C, carbon steel
> – Medium temperature type: 80~200°C, thickened wear-resistant liner
> – High temperature type: 200~400°C, special heat-resistant steel, optional cooling jacket
> Please tell us your material temperature, and we will recommend the most suitable material solution.
Q4: Are there any limits on conveying distance and lifting height?
> Standard design range:
> – Screw conveyor: Single section up to 70 meters; multiple sections can be connected for longer distances
> – Chain conveyor: Single machine up to 60 meters
> – Bucket elevator: Lifting height up to 50 meters
> We can also customize for extra-long distances or special angles. Contact us for detailed solutions.
Q5: Do you provide explosion-proof design?
> Yes. For explosive and flammable conditions such as pulverized coal and biomass dust, we offer:
> – Explosion-proof motors (Ex d IIB T4 standard)
> – Reserved openings for explosion vents / rupture discs
> – Fully sealed structure to prevent dust leakage
> Please specify your explosion-proof rating requirements.
CUSTOMIZATION & MANUFACTURING
Q6: Do you support customization? What is the lead time?
> Over 90% of our equipment is customized according to customer working conditions. Standard models take about 90–120days. Special customizations take 120–180 days, depending on configuration complexity.
Q7: What material options do you offer?
> Common materials include:
> – Carbon steel (Q235B): Standard working conditions
> – Wear-resistant steel (NM400/NM500): Highly abrasive materials
> – Stainless steel 304/316L: Food, chemical, corrosion-resistant requirements
> – Bi-metal wear-resistant composite plate: Extreme abrasion conditions
> We will recommend the most cost-effective material solution based on your material properties.
Q8: What certifications do you have?
> We hold the following certifications:
> – ISO 9001:2015 Quality Management System
> – ISO 14001 Environmental Management System
> – ISO 45001 Occupational Health & Safety Management
> – CE Certification (EN 1090 Steel Structure)
> If you need scanned copies of specific certificates, please contact us.
DELIVERY & LOGISTICS
Q9: Which countries do you export to? Do you have export experience?
> Our equipment has been exported to more than 20 countries worldwide, including:
> – Europe: Germany, France, Poland, Turkey, etc.
> – Southeast Asia: Singapore, Thailand, Indonesia, Vietnam, etc.
> – Middle East: Saudi Arabia, UAE, etc.
> – South America**: Brazil, Chile, etc.
> We are familiar with the full export process: packaging, customs declaration, and ocean freight. We can provide FOB, CIF, and other trade terms.
Q10: What is your packaging method? Is it suitable for long-distance ocean shipping?
> Export-standard packaging:
> – Large items / complete machines**: Rust prevention + waterproof film + fumigated solid wood pallet
> – Precision components: Wooden case with shock-absorbing filling
> – Random accessories: Categorized packing with detailed packing list
> All wooden packaging meets IPPC fumigation standards for direct customs clearance.
Q11: What is your minimum order quantity?
> We do not have a strict minimum order quantity. Single-unit orders are welcome. Bulk orders can enjoy more favorable pricing.
INSTALLATION & AFTER-SALES
Q12: Do you provide installation guidance? Do engineers need to come to site?
> We offer two service options:
> 1. Remote guidance: Detailed installation drawings and operation manuals, video guidance for installation (free of charge)
> 2. On-site service: Dispatch engineers to site for installation and commissioning (travel costs are additional)
> Most customers choose remote guidance. Our equipment is designed as a modular structure for easy installation.
Q13: What is the warranty period? What are the wearing parts?
> Standard warranty period is 12 months (from the date of arrival at port).
> Wearing parts list:
> – Chain / screw flights: Approximately 1–3 years, depending on material abrasiveness
> – Liners: Approximately 2–4 years
> – Bearings: Approximately 2–3 years
> We recommend ordering a wearing-parts spare kit together with your first order.
Q14: How do you solve problems during operation?
> We provide 7×24 technical support:>
> – Response within 24 hours for technical issues
> – Remote video troubleshooting guidance
> – Engineer on-site service when necessary
> – Common spare parts in stock for fast delivery
QUOTATION & COOPERATION
**Q15: How can I get a quote? How long does it take?
> Quotation process:
> 1. You provide material parameters, capacity, installation conditions, and other requirements
> 2. Our engineers evaluate and select the appropriate model
> 3. Formal quotation and technical proposal provided within 7 working days
> You can contact us via email, or the online inquiry form.
Q16: What are your payment terms?
> Standard payment terms:
> – 30% advance payment: After contract signing, to start production
> – 70% balance: Before shipment, or against copy of Bill of Lading
For long-term cooperative customers, more flexible payment terms can be negotiated.
Follow these 3 steps to find your ideal conveyor solution
Step 1: Identify Your Material Type
Different materials require different conveyor designs. Tell us what you are conveying:
| Material Category | Examples | Recommended Conveyor Type |
| Powder / Fine Granules | Fly ash, cement powder, lime powder | Screw Conveyor |
| Small Granules / Pellets | Biomass pellets, plastic granules, grain | Screw Conveyor / Belt Conveyor |
| Fragments / Chips | Wood chips, bark, agricultural residues | Chain Scraper Conveyor |
| Bulky / Abrasive | Bottom ash, slag, MSW, clinker | Chain En-Masse Conveyor |
| Vertical Lift | Any bulk material needs vertical transport | Bucket Elevator |
Step 2: Define Your Working Conditions
Please prepare the following parameters before contacting us:
| Parameter | Why It Matters | Example |
| Capacity (t/h) | Determines conveyor size and power | 10 t/h, 50 t/h, 100 t/h |
| Conveying Distance (m) | Determines machine length | 15m horizontal, 30m incline |
| Incline Angle (°) | Affects capacity and design | 0° horizontal, 30° incline |
| Material Temperature (°C) | Determines material grade | Ambient, 150°C, 300°C |
| Moisture Content (%) | Affects discharge design | Dry, damp, wet (needs dewatering) |
| Abrasiveness | Determines liner thickness | Low, medium, high |
| Application Industry | Determines certification needs | Power plant, cement, mining, recycling |
Step 3: Choose Configuration Options
Based on your answers above, our engineers will recommend:
Material grade — carbon steel / wear-resistant steel / stainless steel
Sealing type — open trough / fully enclosed / gas-tight
Drive system — motor power, gearbox brand, speed range
Auxiliary options — explosion-proof motor, cooling jacket, cleaning device, level sensors
Not Sure Where to Start?
Send us your basic requirements, and our engineers will design a customized solution for you — completely free.
Email: bootec@bootecgroup.com Response time: Within 24 hours
[REQUEST A FREE QUOTATION →]