

Bulk Material Handling: Conveyor Systems
Bulk Material Handling: Conveyor Systems are essential for transporting large quantities of bulk materials across varying distances, orientations, and capacities in industries such as agriculture, mining, construction, power plants, and waste-to-energy facilities. These systems are designed to improve efficiency, safety, and cost-effectiveness.
Types of Conveyor Systems for Bulk Material Handling
1. Belt Conveyors
- Function: Move materials horizontally or on a gentle incline.
- Material Types: Grains, coal, sand, cement, aggregates.
- Features:
- Rubber belts for general materials.
- Heat-resistant or abrasion-resistant belts for specific applications.
- Can include cleats for steep inclines.
- Applications:
- Mining and quarrying for ore and aggregate transport.
- Agricultural use for grain and seed handling.
2. Screw Conveyors
- Function: Move materials using a rotating helical screw blade within a tube.
- Material Types: Powders, granular materials, semi-solid materials.
- Features:
- Can be horizontal, inclined, or vertical.
- Dust-tight designs to prevent material leakage.
- Applications:
- Cement and fly ash transport.
- Food industry for flour and sugar.
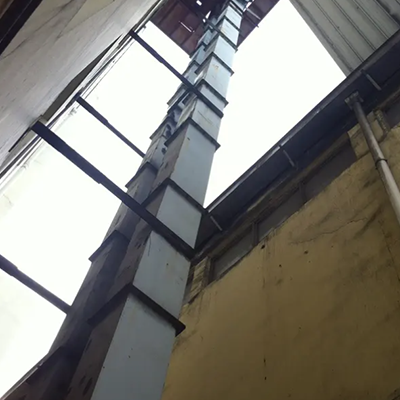
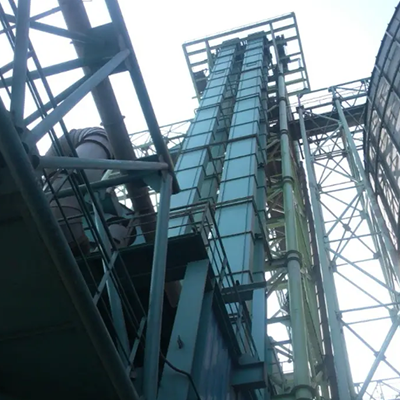
3. Bucket Elevators
- Function: Transport bulk materials vertically or at steep angles.
- Material Types: Fine powders, grains, cement, or coal.
- Features:
- Buckets attached to a belt or chain.
- High capacity and space-efficient.
- Applications:
- Grain silos and cement plants for vertical material transfer.
4. Drag Chain Conveyors
- Function: Move heavy or abrasive materials using a chain-driven system.
- Material Types: Clinker, ash, aggregates, slag.
- Features:
- Enclosed system minimizes spillage and dust.
- Suitable for horizontal or steep incline transport.
- Applications:
- Power plants for ash handling.
- Cement plants for clinker transport.
5. Pneumatic Conveyors
- Function: Use air pressure or vacuum to move fine or lightweight materials through pipes.
- Material Types: Fly ash, grain, cement, or powders.
- Features:
- Enclosed system prevents contamination and spillage.
- Suitable for long-distance transport.
- Applications:
- Power plants for fly ash handling.
- Food and pharmaceutical industries for powder transport.
6. Vibratory Conveyors
- Function: Move materials using vibrating motion.
- Material Types: Granules, powders, or irregularly shaped materials.
- Features:
- Gentle handling for fragile materials.
- Dust-tight options available.
- Applications:
- Recycling and waste processing.
- Food industry for delicate items.
7. Overland Conveyors
- Function: Long-distance transport of bulk materials across open terrain.
- Material Types: Coal, ores, limestone, or aggregates.
- Features:
- Large capacities with energy-efficient designs.
- Minimal environmental impact.
- Applications:
- Mining operations.
- Large-scale cement or aggregate facilities.
8. Telescopic Conveyors
- Function: Adjustable length conveyors for loading and unloading.
- Material Types: Grain, bulk powders, or packaged goods.
- Features:
- Extendable design for flexibility.
- Space-saving and versatile.
- Applications:
- Truck or ship loading and unloading.
Benefits of Conveyor Systems
- Efficiency:
- Continuous material flow reduces downtime and manual labor.
- Cost-Effective:
- Low operating costs compared to other material transport methods.
- Flexibility:
- Can handle diverse materials and be customized for specific needs.
- Safety:
- Reduces risks associated with manual handling and heavy equipment.
- Environmental Compliance:
- Enclosed systems prevent dust emissions and material spillage.
Design Considerations for Conveyor Systems
- Material Properties:
- Flowability, abrasiveness, particle size, and density.
- Capacity:
- Ensure the system can handle the required tons per hour.
- Distance and Orientation:
- Account for horizontal, vertical, or inclined transport needs.
- Environmental Factors:
- Consider operating temperature, humidity, and corrosive conditions.
- Integration:
- Ensure compatibility with existing equipment and processes.
- Maintenance:
- Design systems for easy access and reduced downtime.
Applications of Conveyor Systems in Bulk Material Handling
- Agriculture:
- Grain and seed conveyors, elevators for silos.
- Mining:
- Ore transport from extraction points to processing facilities.
- Cement Industry:
- Handling limestone, clay, clinker, and cement.
- Power Plants:
- Coal and ash conveyors for thermal power generation.
- Waste-to-Energy:
- Bottom ash and fly ash transport systems.
- Food Processing:
- Hygienic conveyors for sugar, flour, or grains.
- Chemical Industry:
- Enclosed conveyors for powders and chemicals.
Technological Advancements in Conveyor Systems
- Smart Conveyor Systems:
- Integrated sensors for real-time performance monitoring.
- IoT-enabled for predictive maintenance.
- Energy-Efficient Designs:
- Variable speed drives to optimize energy use.
- Automated Controls:
- Programmable systems for precise operation.
- Modular Designs:
- Allow easy installation, expansion, and upgrades.
- Environmentally Friendly Features:
- Enclosures and dust suppression systems for cleaner operations.
Example: Waste-to-Energy Plant Conveyor System
- Challenge: Efficiently handle and transport bottom ash and fly ash while meeting environmental regulations.
- Solution:
- Installed drag chain conveyors for bottom ash.
- Pneumatic conveyors for fly ash transfer to silos.
- Dust control systems integrated at transfer points.
- Result:
- Reduced maintenance, improved operational efficiency, and compliance with environmental standards.
Would you like recommendations for a specific type of conveyor system or assistance designing a system for your facility? Let me know the material type, capacity, or specific challenges you’re facing!
SELECTION & TECHNICAL QUESTIONS
Q1: How do I select the right conveyor model? What information should I provide?
> To recommend the most suitable solution, please provide the following details:
> 1. Material type: What material are you conveying? (e.g., fly ash, wood chips, biomass pellets, bottom ash, etc.)
> 2. Material properties: Particle size, temperature, moisture content, abrasiveness
> 3. Capacity requirement: How many tons per hour (t/h) do you need?
> 4. Installation conditions: Conveying distance, incline angle, space limitations
> 5. Application industry: Which industry is this for? (e.g., waste-to-energy plant, biomass power plant, cement plant)
> You can also email us or contact us via WhatsApp. Our engineers will get back to you within 24 hours.
Q2: What is the difference between screw conveyors and chain conveyors? Which one should I choose?
> Both types have different applications:
> – Screw Conveyors: Best for powdery and small-grain materials (e.g., fly ash, cement powder). Good sealing performance, simple structure, low maintenance cost.
> – Chain Scraper Conveyors: Best for bulky, highly abrasive materials (e.g., bottom ash, municipal solid waste, biomass fragments). Supports multiple inlet and outlet points.
> – Bucket Elevators: Ideal for vertical or steep-incline material lifting.
> If you are not sure, tell us your material and working conditions, and our engineers will help you choose.
Q3: Can your equipment handle high-temperature materials? What is the maximum temperature?
> We can customize equipment according to material temperature:
> – Standard type: 0~80°C, carbon steel
> – Medium temperature type: 80~200°C, thickened wear-resistant liner
> – High temperature type: 200~400°C, special heat-resistant steel, optional cooling jacket
> Please tell us your material temperature, and we will recommend the most suitable material solution.
Q4: Are there any limits on conveying distance and lifting height?
> Standard design range:
> – Screw conveyor: Single section up to 70 meters; multiple sections can be connected for longer distances
> – Chain conveyor: Single machine up to 60 meters
> – Bucket elevator: Lifting height up to 50 meters
> We can also customize for extra-long distances or special angles. Contact us for detailed solutions.
Q5: Do you provide explosion-proof design?
> Yes. For explosive and flammable conditions such as pulverized coal and biomass dust, we offer:
> – Explosion-proof motors (Ex d IIB T4 standard)
> – Reserved openings for explosion vents / rupture discs
> – Fully sealed structure to prevent dust leakage
> Please specify your explosion-proof rating requirements.
CUSTOMIZATION & MANUFACTURING
Q6: Do you support customization? What is the lead time?
> Over 90% of our equipment is customized according to customer working conditions. Standard models take about 90–120days. Special customizations take 120–180 days, depending on configuration complexity.
Q7: What material options do you offer?
> Common materials include:
> – Carbon steel (Q235B): Standard working conditions
> – Wear-resistant steel (NM400/NM500): Highly abrasive materials
> – Stainless steel 304/316L: Food, chemical, corrosion-resistant requirements
> – Bi-metal wear-resistant composite plate: Extreme abrasion conditions
> We will recommend the most cost-effective material solution based on your material properties.
Q8: What certifications do you have?
> We hold the following certifications:
> – ISO 9001:2015 Quality Management System
> – ISO 14001 Environmental Management System
> – ISO 45001 Occupational Health & Safety Management
> – CE Certification (EN 1090 Steel Structure)
> If you need scanned copies of specific certificates, please contact us.
DELIVERY & LOGISTICS
Q9: Which countries do you export to? Do you have export experience?
> Our equipment has been exported to more than 20 countries worldwide, including:
> – Europe: Germany, France, Poland, Turkey, etc.
> – Southeast Asia: Singapore, Thailand, Indonesia, Vietnam, etc.
> – Middle East: Saudi Arabia, UAE, etc.
> – South America**: Brazil, Chile, etc.
> We are familiar with the full export process: packaging, customs declaration, and ocean freight. We can provide FOB, CIF, and other trade terms.
Q10: What is your packaging method? Is it suitable for long-distance ocean shipping?
> Export-standard packaging:
> – Large items / complete machines**: Rust prevention + waterproof film + fumigated solid wood pallet
> – Precision components: Wooden case with shock-absorbing filling
> – Random accessories: Categorized packing with detailed packing list
> All wooden packaging meets IPPC fumigation standards for direct customs clearance.
Q11: What is your minimum order quantity?
> We do not have a strict minimum order quantity. Single-unit orders are welcome. Bulk orders can enjoy more favorable pricing.
INSTALLATION & AFTER-SALES
Q12: Do you provide installation guidance? Do engineers need to come to site?
> We offer two service options:
> 1. Remote guidance: Detailed installation drawings and operation manuals, video guidance for installation (free of charge)
> 2. On-site service: Dispatch engineers to site for installation and commissioning (travel costs are additional)
> Most customers choose remote guidance. Our equipment is designed as a modular structure for easy installation.
Q13: What is the warranty period? What are the wearing parts?
> Standard warranty period is 12 months (from the date of arrival at port).
> Wearing parts list:
> – Chain / screw flights: Approximately 1–3 years, depending on material abrasiveness
> – Liners: Approximately 2–4 years
> – Bearings: Approximately 2–3 years
> We recommend ordering a wearing-parts spare kit together with your first order.
Q14: How do you solve problems during operation?
> We provide 7×24 technical support:>
> – Response within 24 hours for technical issues
> – Remote video troubleshooting guidance
> – Engineer on-site service when necessary
> – Common spare parts in stock for fast delivery
QUOTATION & COOPERATION
**Q15: How can I get a quote? How long does it take?
> Quotation process:
> 1. You provide material parameters, capacity, installation conditions, and other requirements
> 2. Our engineers evaluate and select the appropriate model
> 3. Formal quotation and technical proposal provided within 7 working days
> You can contact us via email, or the online inquiry form.
Q16: What are your payment terms?
> Standard payment terms:
> – 30% advance payment: After contract signing, to start production
> – 70% balance: Before shipment, or against copy of Bill of Lading
For long-term cooperative customers, more flexible payment terms can be negotiated.
Follow these 3 steps to find your ideal conveyor solution
Step 1: Identify Your Material Type
Different materials require different conveyor designs. Tell us what you are conveying:
| Material Category | Examples | Recommended Conveyor Type |
| Powder / Fine Granules | Fly ash, cement powder, lime powder | Screw Conveyor |
| Small Granules / Pellets | Biomass pellets, plastic granules, grain | Screw Conveyor / Belt Conveyor |
| Fragments / Chips | Wood chips, bark, agricultural residues | Chain Scraper Conveyor |
| Bulky / Abrasive | Bottom ash, slag, MSW, clinker | Chain En-Masse Conveyor |
| Vertical Lift | Any bulk material needs vertical transport | Bucket Elevator |
Step 2: Define Your Working Conditions
Please prepare the following parameters before contacting us:
| Parameter | Why It Matters | Example |
| Capacity (t/h) | Determines conveyor size and power | 10 t/h, 50 t/h, 100 t/h |
| Conveying Distance (m) | Determines machine length | 15m horizontal, 30m incline |
| Incline Angle (°) | Affects capacity and design | 0° horizontal, 30° incline |
| Material Temperature (°C) | Determines material grade | Ambient, 150°C, 300°C |
| Moisture Content (%) | Affects discharge design | Dry, damp, wet (needs dewatering) |
| Abrasiveness | Determines liner thickness | Low, medium, high |
| Application Industry | Determines certification needs | Power plant, cement, mining, recycling |
Step 3: Choose Configuration Options
Based on your answers above, our engineers will recommend:
Material grade — carbon steel / wear-resistant steel / stainless steel
Sealing type — open trough / fully enclosed / gas-tight
Drive system — motor power, gearbox brand, speed range
Auxiliary options — explosion-proof motor, cooling jacket, cleaning device, level sensors
Not Sure Where to Start?
Send us your basic requirements, and our engineers will design a customized solution for you — completely free.
Email: bootec@bootecgroup.com Response time: Within 24 hours
[REQUEST A FREE QUOTATION →]